As a C Type Welding Machine supplier who has worked with dozens of manufacturing facilities over the past 7 years, I’ve seen firsthand how even small tweaks to the welding process can cut production time by 15% or reduce material waste by 10%—without requiring expensive new equipment. Our C Type machines are built for consistency, but their performance only shines when operators and maintenance teams optimize every step of the workflow around them. C Type Welding Machine
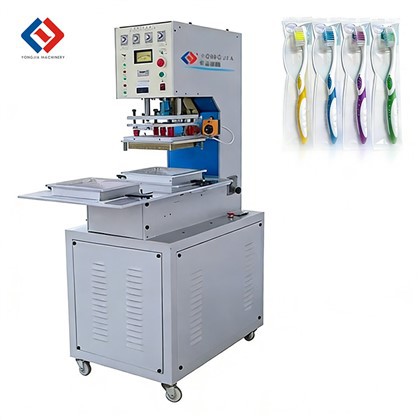
I still remember a shop in rural Ohio that bought two of our C Type welders two years ago. For the first 6 months, they were treating the machines like “set-it-and-forget-it” tools: they used the same welding parameters for every part, never calibrated the machine, and let their 3-year-old rolls of welding wire run out until they had to replace them mid-shift. Their welds had a 8% rejection rate, and they were falling behind on orders for agricultural equipment frames. After we walked their team through a process optimization deep dive, that rejection rate dropped to 1.2% in 3 months, and their weekly output went up by 22%. That kind of transformation isn’t magic—it’s about applying intentional, data-driven steps to work with your C Type welding machine, not against it.
Let’s break down the key areas to optimize, tailored specifically for C Type machines (also called C-frame or gap frame welders, which are distinct from linear welders or robotic arms because of their fixed, compact frame design perfect for spot welding, projection welding, and even some custom arc welding jobs).
First, master parameter calibration for your specific application. C Type machines get their precision from matching three core parameters: current voltage, weld time, and electrode force. But the mistake I see most often is using generic parameters from a machine manual or a past job instead of calibrating for the exact material and part thickness you’re working with. For example, a customer welding 16-gauge steel for storage rack brackets needs a different set of settings than a customer welding 12-gauge aluminum for automotive door hinges. The manual might say 1000 amps, 0.2 seconds, 200 lbs of force, but that’s a one-size-fits-all baseline—not a tailored setting. We recommend our clients run a “test weld series” before every production run: make 5 test welds on scrap material matching their production parts, adjust parameters until the weld has a smooth, uniform penetration (no burn-through on thin material, no incomplete fusion on thick material), and log those numbers in a shared spreadsheet. That log becomes your reference for future runs, and it cuts down on trial-and-error time during production. Also, don’t forget to update parameters when your material supplier changes: even a 0.005-inch difference in steel thickness can throw off a weld if your settings don’t adjust.
Next, optimize electrode maintenance and replacement. Electrodes are the workhorses of C Type machines—they make direct contact with the workpiece, so their condition directly impacts weld quality. Over time, electrodes wear down, get dirty, or form “mushroom caps” from repeated heat and pressure. A worn electrode will create uneven force, leading to weak welds, or leave marks on the workpiece that require extra finishing work. Here’s a simple routine we train our customers to follow: after every 500 welds, inspect the electrode tips for discoloration, spatter buildup, or deformation. If there’s spatter, use a wire brush or electrode cleaning tool (we sell budget-friendly ones as part of our machine accessory line) to remove buildup. If the tip has a mushroom shape, dress it with an electrode grinder to restore its flat, uniform surface. We also recommend a rule of thumb for replacement: replace electrodes when their diameter wears down by 10% (e.g., a 5mm electrode becomes 4.5mm) or every 20,000 welds, whichever comes first. Skipping electrode maintenance costs one of our regular clients $1,200 a month in rework and material waste—numbers that add up fast.
Then, streamline workflow around the C Type machine. C Type machines are fast, but bottlenecks happen when the machine is waiting for parts, wire, or maintenance. Let’s go back to that Ohio agricultural shop: their team would load parts, then wait 10 minutes for new wire spools, or hunt for a specific part jig when changing production runs. The fix here is simple: pre-stage parts and materials 10 feet or less from the C Type welder, so operators don’t waste time walking back and forth. For production changeovers, use jigs and fixtures specifically designed for your parts—our team provides custom jig design consultations for all our clients, because a proper jig cuts changeover time from 15 minutes to 3 minutes. Another workflow tweak: group identical parts into production batches. If you’re running 1,000 of one bracket and 500 of another, complete all 1,000 first before switching settings, instead of alternating. This reduces the number of test welds you need to run and keeps the machine in production mode, not setup mode. We’ve seen shops cut their total production time per part by 20% just by rearranging their workstations around the C Type welder, not the other way around.
Don’t overlook power supply and machine environment optimization. C Type welders rely on consistent electrical power to deliver stable current and force. If your shop has old wiring, or too many machines drawing power at once during peak shifts, your C Type welder’s performance will drop—you might see inconsistent welds even when your parameters are perfect. We recommend hiring an electrician to test your shop’s power supply quarterly, and make sure your C Type machine is on a dedicated circuit (not shared with other heavy equipment like forklift chargers or CNC mills). Also, keep the area around the C Type welder clean and temperature-controlled. Dust, oil, and extreme temperatures (above 90°F or below 32°F) can affect the machine’s internal components and lead to premature wear. One client in Texas was seeing 20% more machine downtime during summer months—turns out their welder was placed near a loading dock where heat built up; moving it to a shaded, well-ventilated area cut downtime by 18% within a month.
Now, data tracking and continuous improvement. The best part of optimizing your C Type welding process is that small, regular adjustments add up over time. We encourage our clients to log three key data points for every production run: number of welds, number of rejections, and any machine issues (e.g., electrode wear, power drops). Use a simple notebook, a spreadsheet, or even a basic app—you don’t need complex industrial software. Every month, set aside 30 minutes to review that data. Look for patterns: if you’re seeing more rejections on Wednesdays, check if power is weaker that day. If electrodes wear out twice as fast when welding aluminum, adjust your dressing schedule. One automotive client used this method to discover that they were welding aluminum at a lower force than needed, so they increased force slightly and extended electrode life by 30%. This isn’t a one-time fix—it’s a cycle of checking, adjusting, and improving that keeps your C Type machine performing at its best.
Of course, no optimization works without proper operator training. I’ve visited shops where the C Type machine is sitting unused because the operator doesn’t know how to adjust parameters or maintain electrodes. When you invest in a C Type welding machine (and we offer flexible financing options to fit small and large shops alike), we provide on-site training for your team, plus access to our 24/7 technical support line. We also recommend that operators log their own observations—after all, they’re the ones using the machine every day, and they’ll notice small issues that a maintenance team might miss. Encourage your team to ask questions: if something feels off about a weld, don’t wait to check it. That kind of proactive approach is the biggest driver of a successful optimized process.
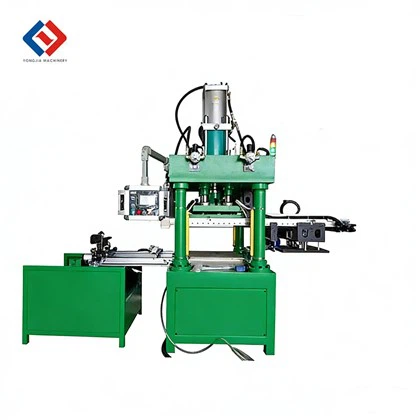
If you’re ready to turn inconsistent welds, wasted material, and delayed orders into a smoother, more profitable production line, our team is here to help. We can walk you through a custom process assessment, help you calibrate your C Type machine, and provide the tools and support you need to keep your welding process running at peak efficiency. Reach out to our team to learn more about how our C Type welding machines and optimization services can work for your facility.
HF Welding Machine References:
- Welding Process Optimization: A Practical Guide, American Welding Society, 2021
- C-Type Welder Maintenance Best Practices, Fabricating & Metalworking Magazine, Volume 56, Issue 3, 2022
- Material Consistency and Weld Quality Correlation, Journal of Manufacturing Processes, Volume 45, 2020
- Workflow Optimization for Compact Welding Machines, Small Shop Manufacturing Association, 2021
Dongguan Yongjia Machinery Equipment Co., Ltd.
We are one of the most reliable c type welding machine manufacturers and suppliers in China, specialized in providing high quality customized service. Please feel free to wholesale advanced c type welding machine at low price from our factory. For quotation, contact us now.
Address: No. 240, Chashan South Road, Chashan Town, Dongguan City, Guangdong Province, China
E-mail: info@yjwelding.com
WebSite: https://www.yjhighfrequencymachine.com/
