If you’re in the market for turbine flow meters—say, for water processing, chemical manufacturing, or even oil & gas—you probably already know these bad boys are workhorses for reliable, accurate flow measurement. But here’s the thing: I’ve worked with hundreds of clients over the years who come back to me saying, “My meter worked fine for the first six months, now it’s all over the place.” Nine times out of ten? Fluid contaminants are the culprit. As a turbine flow meter supplier, I’ve spent way too much time troubleshooting these issues, and today I’m breaking down exactly what that gunk in your fluid does to throw your meter off, why it matters, and what you can do to fix it. Turbine Flow Meter
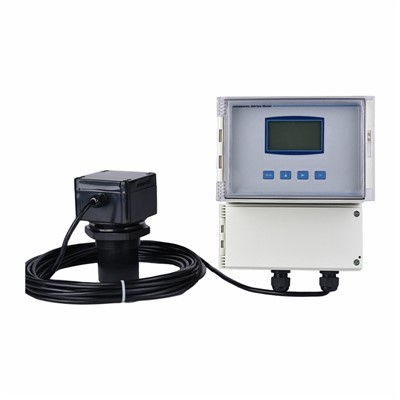
First, let’s cut through the jargon for a sec. Turbine flow meters work on that simple principle: fluid flows through the meter’s housing, spins a turbine rotor inside, and the faster the flow, the faster the rotor spins. A pickoff sensor (usually magnetic) counts those spins, translates them into a flow rate, and bam—you’ve got your number. The entire system relies on the rotor spinning smoothly, evenly, and at a speed that directly matches the volumetric flow of the fluid. Any contaminant in that fluid messes with one of those parts, and suddenly your readings are wrong.
Not all contaminants are created equal, either. I see three main types that pop up constantly: solid particulates (think sediment, rust, metal shavings, or even tiny plastic bits), liquid contaminants (like oil, water, or glycol that shouldn’t be mixed into your base fluid), and gaseous contaminants (air bubbles, vapor, or dissolved gases that come out of solution when pressure drops). Each hits the meter differently, and none of them are good. Let’s dive into each one’s effect, because that’s where most people get tripped up.
Starting with solid particulates—this is the big one for industrial applications where piping is old, or fluid isn’t filtered properly. I once had a client at a food processing plant who didn’t install a pre-filter on their meter for their syrup line. After three months, their meter was reading 15% higher than actual flow. When we pulled the meter apart, there was a 2mm chunk of rust jammed between the rotor blades and the housing. That chunk didn’t stop the rotor entirely, but it created extra friction, making it spin faster than it should for the actual flow. So their “high accuracy” readings were totally off because the gunk was slowing the rotor slightly? Wait, no—wait, let’s get that right. If particulates get caught on the rotor, they add drag, so to keep up with the flow, the rotor spins faster to overcome that drag. That makes the sensor count more spins than it should, so the flow rate calculation (which is spin count vs flow) is inflated. That’s called “high registration error,” and it’s super common with unfiltered solid particulates.
Worse yet, fine abrasives—like silica sand or metal filings—act like sandpaper on the rotor and the bearing surfaces. Over time, that wears down the blades until their shape is altered. I had another client in a chemical plant with a meter for corrosive acid; their piping had started corroding, so tiny iron particles were in the acid. After a year, the rotor blades were rounded from abrasion, so the drag on the rotor was less. Now it spun slower for the same flow, leading to low registration error—readings that were 10% lower than actual flow. That’s a nightmare for inventory control, or for billing if you’re measuring fluid you sell to a third party. Even smaller particulates, like silt or lint (yes, lint in water lines—don’t ask), can build up on the meter’s inlet straightening vanes. Those vanes are there to make the fluid flow straight before it hits the rotor; if they’re clogged with gunk, the fluid swirls, so the rotor spins unevenly. That causes fluctuating readings, like your meter jumps 5% one minute, drops 7% the next, for no apparent reason.
Now liquid contaminants—this is a tricky one because it’s easy to miss if your fluid is supposed to be single-phase. The most common liquid contaminant I see is entrained oil in water lines, or water in oil lines. Let’s take oil in water first: oil is less viscous than water, right? So if you have a mix, the lubrication on the rotor bearings (usually fluid itself, or a tiny amount of grease) gets mixed with the oil, making it slippier. Wait, no—wait, for meters that measure low-viscosity fluids, adding a less viscous contaminant makes the total fluid less viscous, so the rotor spins faster for the same flow. That’s high error again. On the flip side, if you have a thicker liquid contaminant, like glycol mixed into gasoline, that increases the fluid’s viscosity. Higher viscosity means more drag on the rotor, so it spins slower for the same flow—low error. But here’s the curveball: if the liquid contaminant is immiscible (meaning it doesn’t mix, like oil and water), it can form droplets that get stuck in the rotor’s blades. Similar to solid particulates, that adds drag, making the rotor spin faster. I had a HVAC client once who had a 1000L water line that accidentally got a small leak in a diesel pipe nearby. The diesel droplets would build up in the rotor, then get pushed out randomly, so their meter readings bounced by up to 8% every time a droplet dislodged. That’s not just bad accuracy—it’s inconsistent, which makes it useless for any process control.
Then there are gaseous contaminants, which I’d say are the most underrated problem. Air bubbles in the line, especially for liquid flow meters. Let’s break this down: if you’re measuring a liquid, air takes up space, so the actual liquid flow rate is lower than the total volume the meter is counting (since the meter counts all fluid, liquid + air). That leads to low registration error—readings that are lower than actual liquid flow. But if there’s a lot of air, it can push the rotor instead of the liquid, making it spin erratically. I once worked with a municipal water utility that had a meter on a new line; they forgot to purge air out of the piping before startup. For the first two weeks, their meter was spitting out readings that were almost 20% lower than actual, because the air bubbles were taking up half the line. Vapor is even worse—like when volatile fluid (propane, for example) drops in pressure, turns to vapor, and creates gas pockets. Those vapor pockets can cause the rotor to stall temporarily, then spin super fast when the pocket passes, leading to wild fluctuations. Even dissolved gases that come out of solution downstream (like nitrogen in water lines) can build up in the top of the meter’s housing, creating a pocket that disrupts flow. And if you’re measuring gas flow? Wait, no—turbine meters for gas are a different beast, but even then, liquid contaminants (like condensation) will throw off readings. I’ve seen gas turbine meters get 12% error just from a small condensation puddle on the rotor blades.
Now, let’s talk about long-term effects, not just immediate errors. I mentioned abrasion earlier, but corrosion is another big one, especially if the contaminant is corrosive (like chloride ions in water, or acid in process lines). Corrosion eats away at the meter’s housing, rotor, and bearings, leading to play in the rotor shaft. If the shaft has play, the rotor wobbles, so its spin speed doesn’t line up with flow rate anymore. That leads to both high and low error, and eventually, the rotor will start scraping against the housing, which can cause total failure if you don’t catch it. I had a manufacturing client who went six months without calibrating their meter because it “was working fine” during initial setup. When we pulled it apart, the rotor was worn so bad that it was scraping the housing, and readings were off by 18%—enough to cost them thousands of dollars in overpaid fluid bills and bad product batches.
Wait, but as a supplier, we don’t just yell about problems—we also have actual fixes, right? A lot of clients ask, “Do I just replace my meter every time there’s gunk?” No, that’s the lazy answer. Let’s go through the solutions tailored to the contaminant type. For solid particulates: first, add a pre-filter. That’s the easiest, cheapest fix. We supply line-mounted strainers right alongside our turbine meters, sized to match your pipe diameter and the size of particulates you expect. If you’re dealing with fine abrasives, you might also want a cartridge filter downstream of the strainer, to catch smaller bits. For liquid contaminants: install a separator. We work with a couple of reputable separator vendors to offer inline oil-water separators for our clients, or for immiscible liquid droplets, a coalescing filter that pulls those out before they hit the meter. For gaseous contaminants: air purgers—simple devices that vent air pockets out of the top of the meter housing, or install a pressure regulator upstream to keep fluid pressure stable, so dissolved gases don’t come out of solution.
Also, regular maintenance—way cheaper than replacing a meter or fixing a process error. We recommend annual inspections, or bi-annual if you’re in a dirty, high-contaminant environment. When we do inspections, we check for rotor wear, bearing play, and clean any build-up on the straightening vanes. A quick clean and calibration takes 30 minutes, and it can save you way more than the cost of the service in avoided errors. I always tell clients: if your meter is reading differently than it did when you first installed it, don’t just blame the meter—first check the fluid quality. 9 times out of 10, contaminants are the root cause, not a bad meter.
Wait, let’s make sure I didn’t miss a common scenario. What about low-flow applications? Turbine meters are great for low to medium flow, but if you have very low flow, even tiny contaminants can stall the rotor. I had a client with a micro-turbine meter for a medical gas line—they had a tiny bit of moisture in the line, and it froze in the rotor bearing, stopping the meter entirely. That’s a extreme, but it’s a good example of how even small contaminants can hit specialized applications.
Another thing: calibration. A lot of people don’t realize that turbine meters need to be calibrated for the specific fluid they’re measuring. If you calibrate a meter for clean water, then use it on water with sediment, it’s already going to be off. But if you account for the expected contaminants during calibration? You can adjust the spin vs flow ratio to compensate for drag from particulates or liquid contaminants. That’s a service we offer, too—custom calibration for clients who know they’ll have controlled levels of contaminants.
Let me wrap this up with a real example that sticks with me. Last year, a craft brewery came to us panicking. Their turbine meter for their beer wort line was reading 12% lower than actual flow, so they were brewing 10% less beer than their recipe called for. That cost them thousands in wasted ingredients and lost sales. We tested their fluid, found fine yeast particles and malt sediment in the wort, which were sticking to the rotor blades, making it spin slower. We installed a 100-micron pre-filter on their line, cleaned the meter, and recalibrated it. Now their readings are within 0.5% accuracy, and they haven’t had an issue since. That’s exactly why I do what I do—helping people avoid those costly mistakes.
At the end of the day, turbine flow meters are reliable, but they’re not unbreakable. Fluid contaminants aren’t a flaw in the meter design—they’re a reality of industrial and commercial fluid systems. If you’re seeing inconsistent readings, weird fluctuations, or readings that drift over time, the first thing to check isn’t your meter’s calibration (though that matters) — it’s what’s actually in your fluid.
If you’re dealing with flow measurement issues, or you’re looking to upgrade to a meter that can handle your specific fluid conditions, reach out to our team to talk through your needs. We can help you size the right meter, add any necessary filters or separators, and set up a maintenance schedule to keep your readings accurate for years. It’s way better to nip the contaminant problem in the bud than to deal with costly errors down the line.
Wireless Digital Dynamometer References
- Miller, R. W. (2004). Flow Measurement Engineering Handbook (3rd ed.). McGraw-Hill.
- ISO 9951:2016, Measurement of fluid flow in closed conduits — Turbine meters. International Organization for Standardization.
- Spitzer, D. W. (2003). Industrial Flow Measurement. ISA – The Instrumentation, Systems, and Automation Society.
- Garvey, S. J., & Atkinson, C. (2018). Effects of solid particulates on turbine flow meter performance. Flow Measurement and Instrumentation, 62, 112-119.
- Richardson, J. F., Harker, J. H., & Backhurst, J. R. (2002). Chemical Engineering Volume 2: Particle Technology and Separation Processes. Butterworth-Heinemann.
Dalian Yheng Technology Co., Ltd.
Dalian Yheng Technology Co., Ltd. is one of the leading turbine flow meter manufacturers and suppliers in China, also supports customized service. We warmly welcome you to buy high quality turbine flow meter in stock here from our factory. Contact us for more details.
Address: F1605, NO.10 Huoju road, High-tech Industrial Zone, Dalian, China
E-mail: admin@dlyheng.com
WebSite: https://www.yhengphmeter.com/
